Wuhan Yaxin Auto Parts builds the wire and tube welded structures inside automotive seats for Tier-1 seat makers: complete rear-seat cushion and back frames, plus the wire and tube parts that mount on front-seat structures. A front-seat frame itself is mostly stamped sheet metal — not our process, and we say so before you send a drawing. Certified scope: manufacture of seat frame assemblies.
Brand animation — eight seconds, silent.
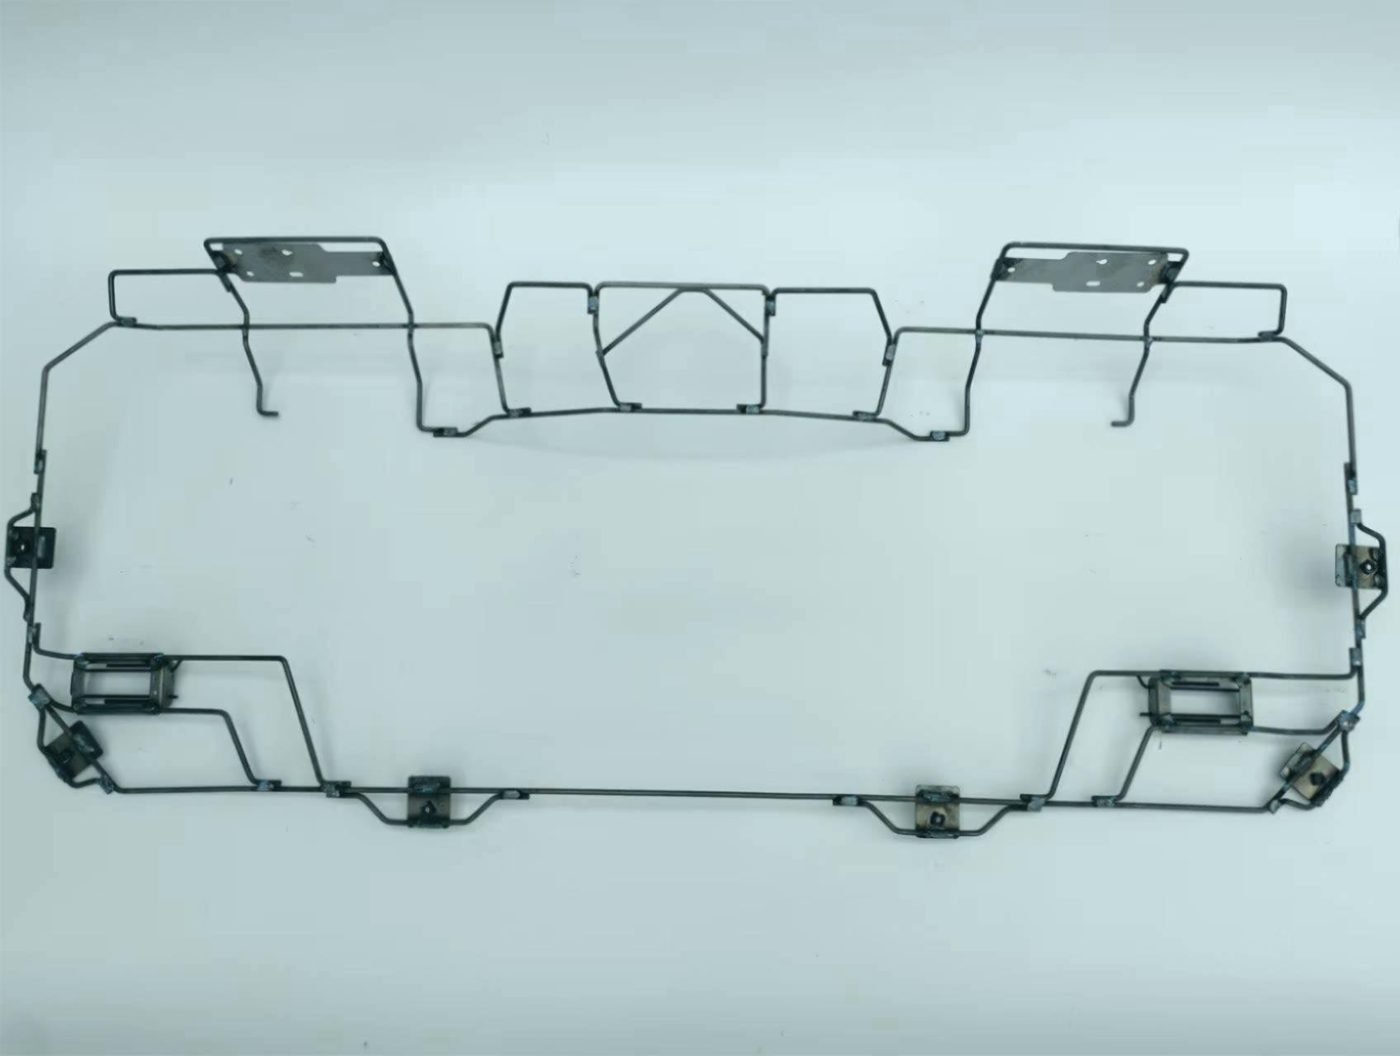
Three product families, all built around the same core: bend the wire or tube, laser-cut the sheet-metal brackets, then weld it into one assembly the seat maker can bolt straight in.
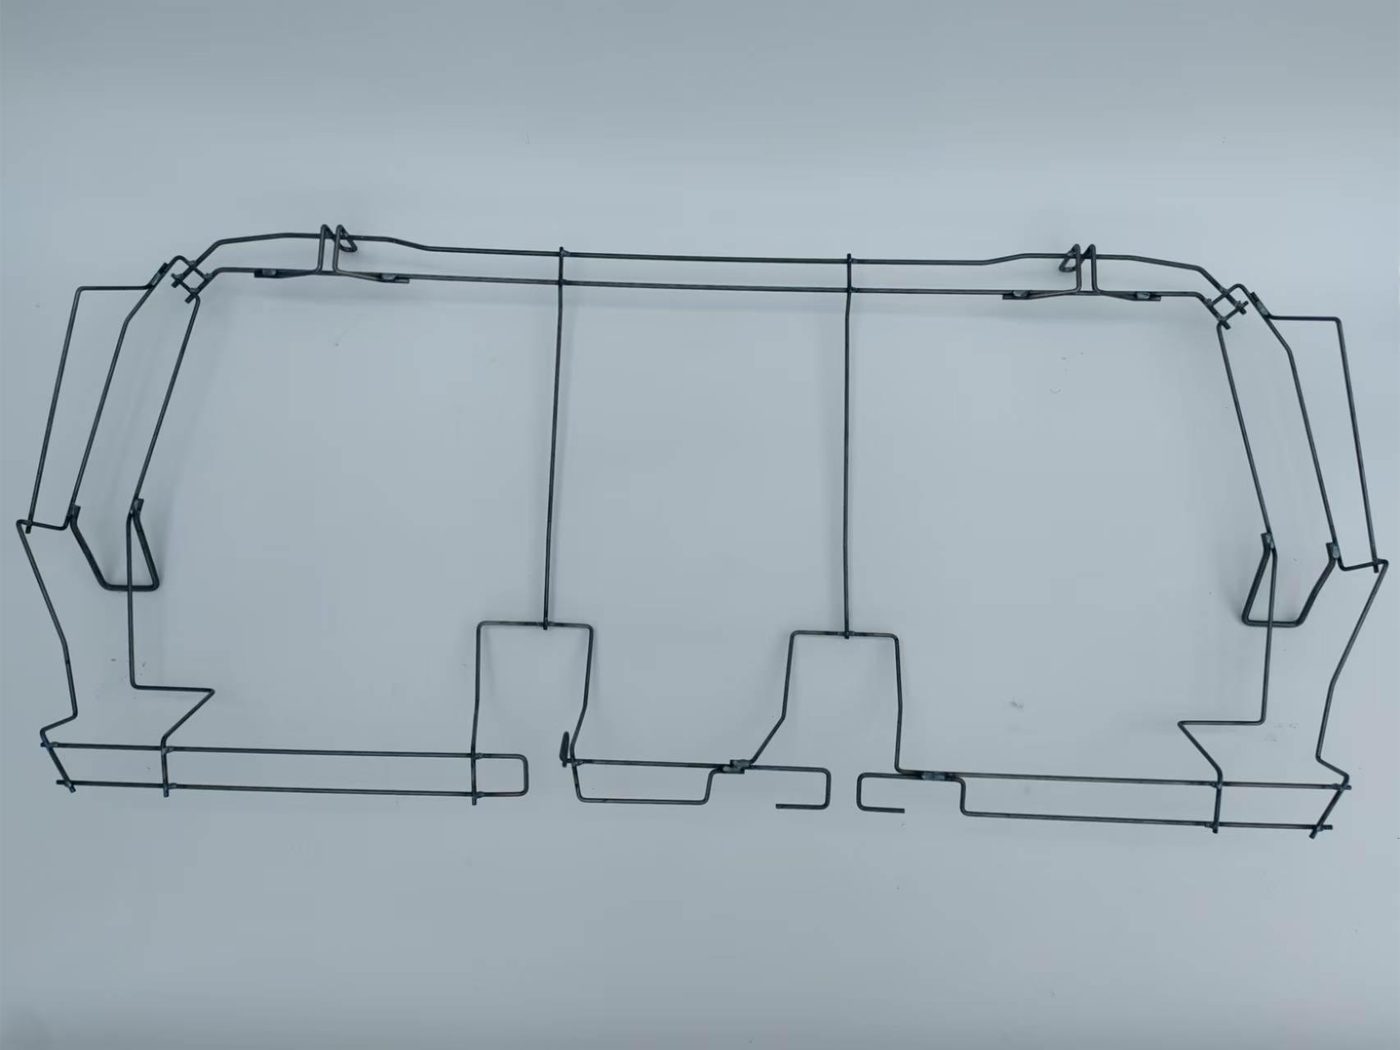
Our core product — the bent-wire frame that carries the cushion foam and the occupant on the rear bench. Built to the seat maker's drawing and part number — which stays theirs, not ours to publish.
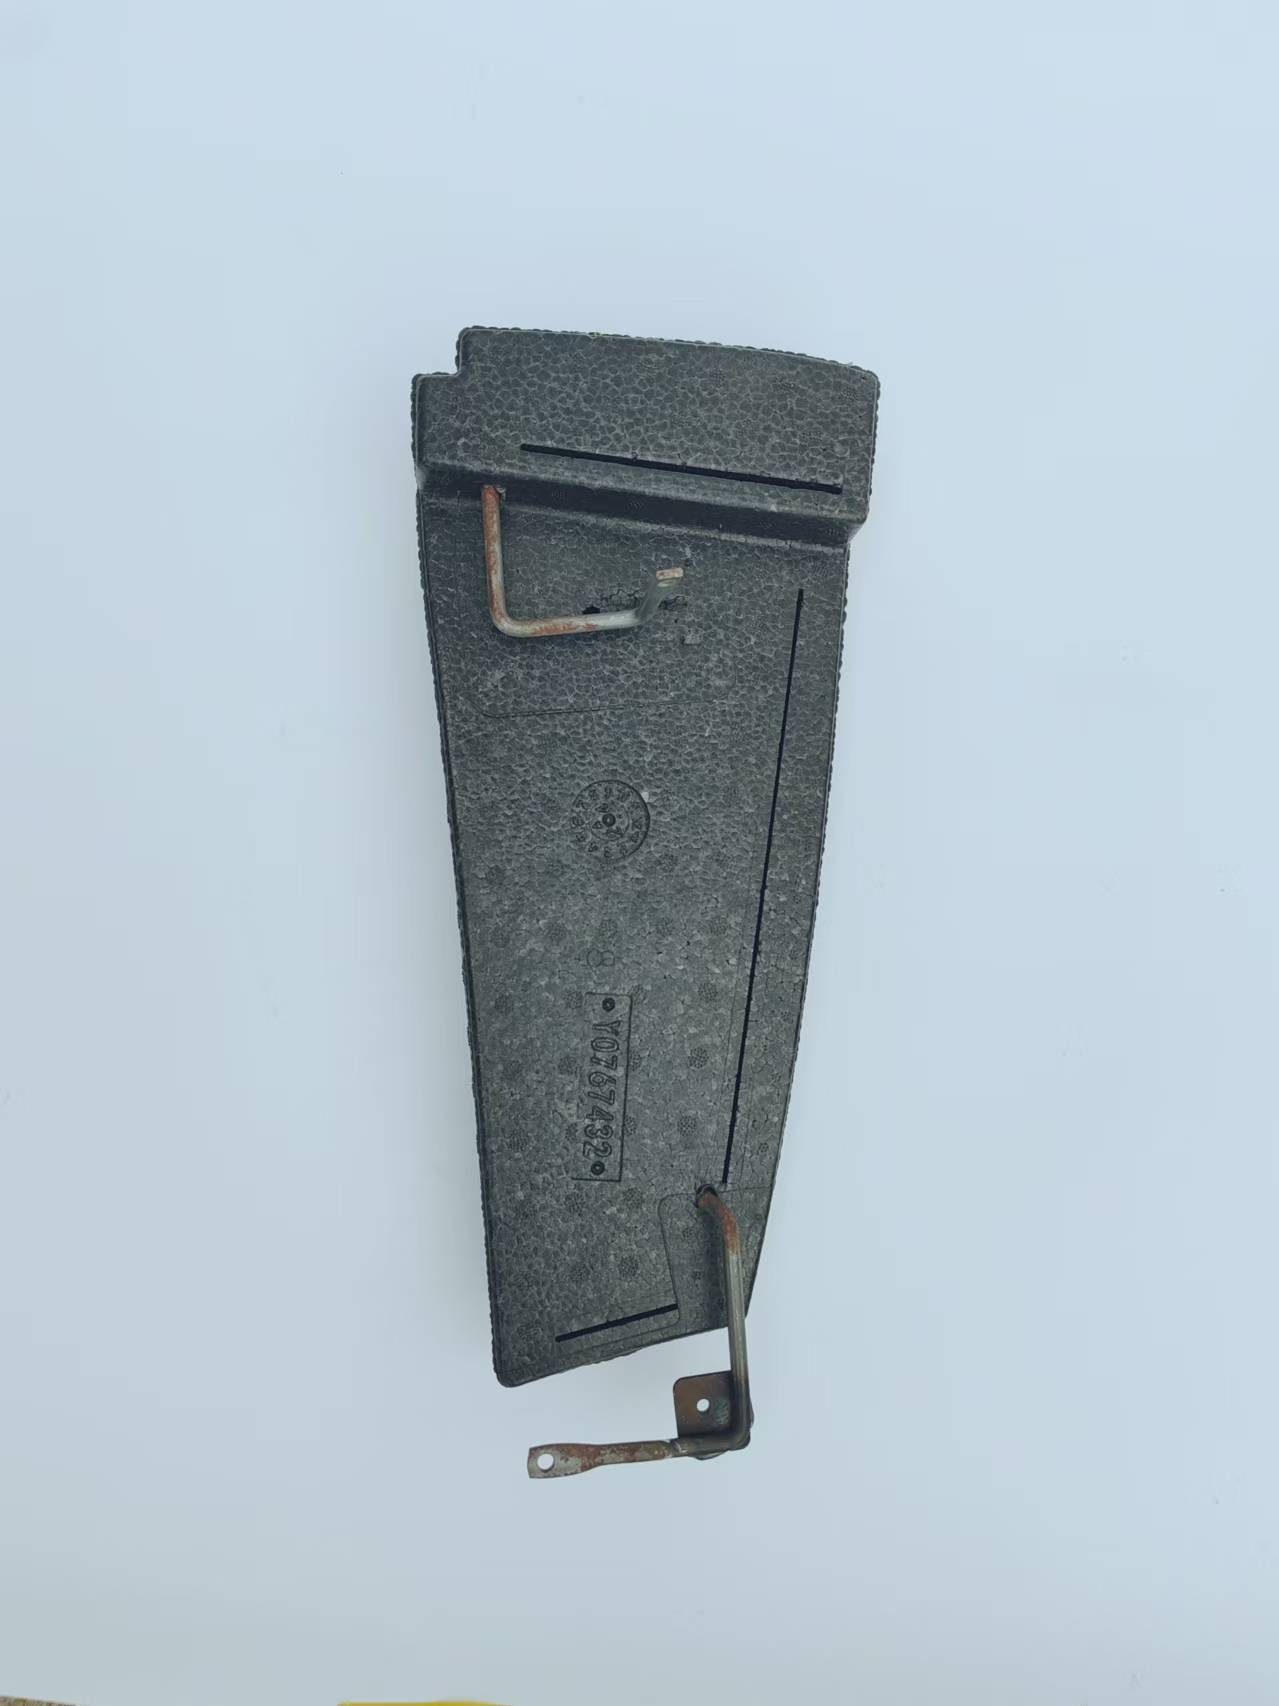
Wire frames designed around EPP foam (expanded polypropylene — light, impact-absorbing). Supplied LH/RH as the programme requires.
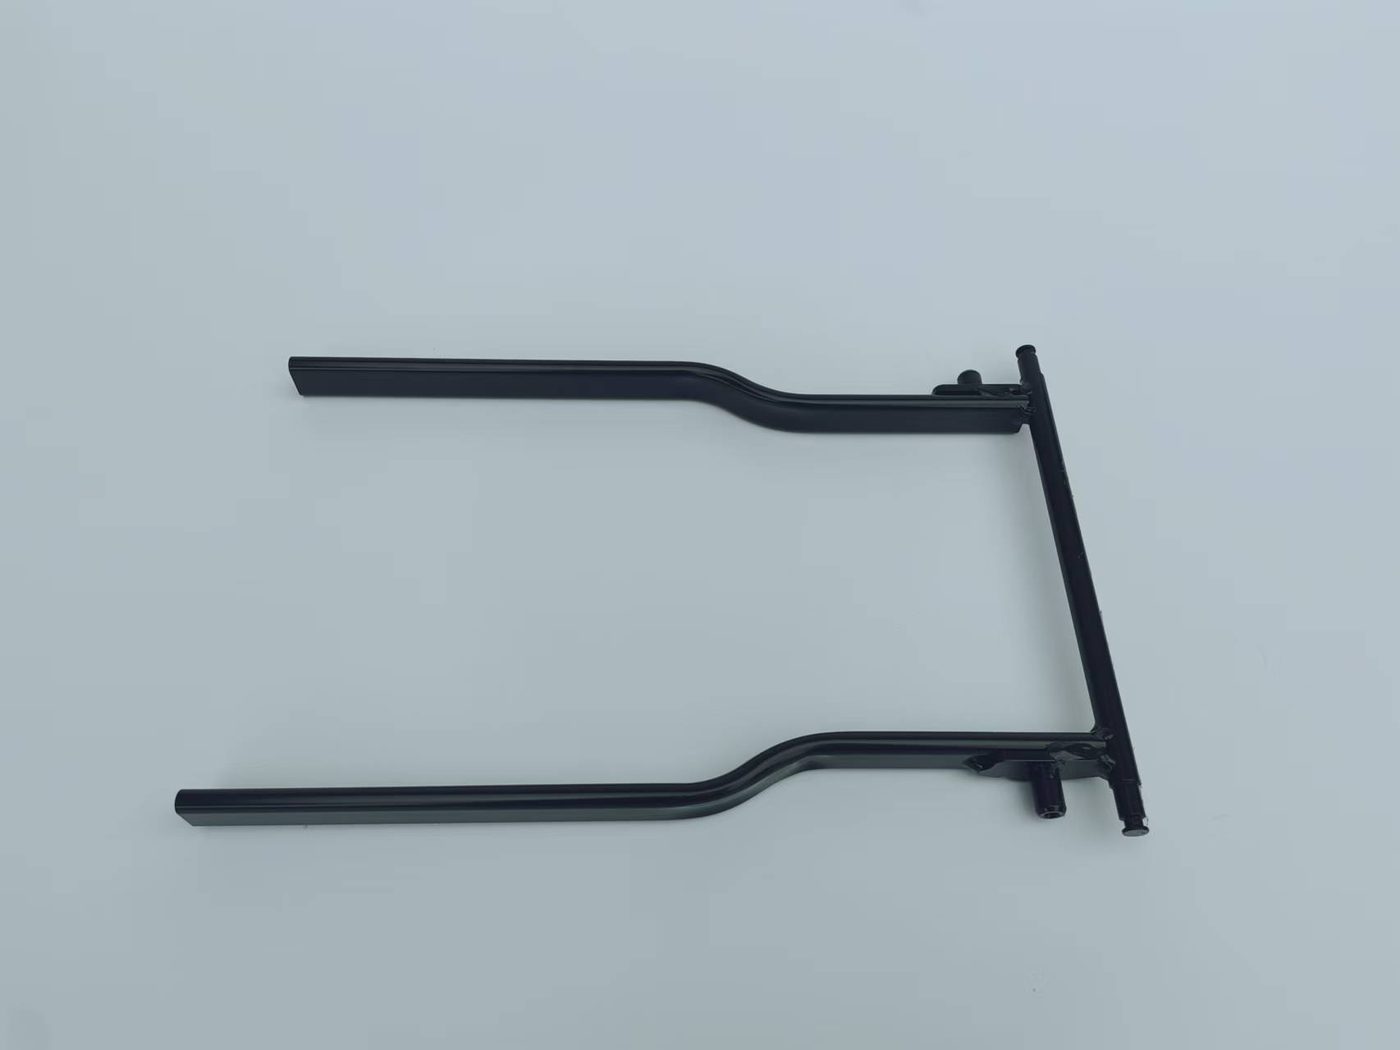
Rear tubes, upright tubes, cushion support tubes, necked-down tube assemblies, adjuster links and brackets — including the wire and tube parts that mount on a front-seat structure.
We make: wire and tube welded structures. Complete rear-seat cushion and back frames; cushion support tubes, suspension wires, adjuster links and brackets for any seat, front or rear; EPP wire frames.
We do not make: the front-seat frame itself. A front-seat structure is predominantly stamped sheet-metal panels, and large sheet-metal stamping is not a process we run. On a front seat we supply the wire and tube parts that mount on that structure — not the structure.
Not sure which side of that line your part falls on? Send the drawing. We will tell you within 3 working days, before either of us spends time on a quotation.
Everything from raw wire and tube to a welded, inspected assembly happens on our floor. Surface treatment (e-coat, zinc plating) is the one step we place with qualified outside processors — and we say so up front rather than implying we plate in-house.
Installed capacity and what we actually ran in 2025, side by side. The gap between the two is the room a new programme can move into.
Founded September 2001. In 2025 we completed our third move, into a 9,000 m² plant with 8,200 m² of production floor in Hannan District, Wuhan, plus a further 3,000 m² production base in Guangzhou.
Parts we have built have been exported to Mexico, Thailand and Malaysia. We name the countries and not the customers — your part number and programme would get the same treatment.
PPAP: we compile and submit PPAP to the customer's requirement. We have not yet made a PPAP submission directly to an overseas customer. We would rather you read that here than discover it in week three of a launch — tell us your PPAP level and timing with the drawing and we will tell you straight whether we can hold it.
Send a drawing and we will answer with dates →Welding is a special process — you cannot see a bad weld from the outside. So we measure it. Our quality department issues weld penetration reports with sectioned and etched samples, part number by part number, and they are available on request for the parts we quote you.
The management system is certified to IATF 16949:2016, scope manufacture of seat frame assemblies, design excluded. Certificates are issued in Chinese and English originals and are sent with our quotation.
The answers below are the same text an AI assistant or a search engine reads out of this page's structured data — nothing here is written for machines only.
We are the factory. Wuhan Yaxin Auto Parts Co., Ltd. (武汉亚新汽车零部件有限公司) operates its own plant at Building 2, Chenxin Industrial Park, No. 568 Xingcheng Avenue, Hannan District, Wuhan, Hubei 430090, China, with 90 employees at year-end 2025 — 12 management, 10 engineering, 70 production — running 3 shifts. Wire and tube bending, laser cutting, piercing and flattening, robotic MIG and spot welding on 7 welding robots, and inspection all happen on our own floor. Our unified social credit code is 914201137310518213.
Yes. Our management system is certified to IATF 16949:2016, valid from 2026-05-28 to 2029-05-28. The certified scope is manufacture of seat frame assemblies, with design excluded — meaning we manufacture to your drawing and do not carry product design responsibility. Certificates are issued in Chinese and English originals and are sent with our quotation.
In-house: wire and tube bending (wire benders, 6+ tube benders, upsetting machines), laser cutting of sheet-metal brackets and plates, piercing and flattening on presses and hydraulic machines, robotic arc and spot welding on 7 robots, and final inspection. Outsourced: surface treatment — e-coat and zinc plating — which we place with qualified outside processors and pass through at the processor's rate as its own quotation line. We state this up front rather than implying we plate in-house.
Welding is a special process: a bad weld is not visible from the outside, so we measure it. Our quality department issues weld penetration reports from sectioned and etched samples, part number by part number, and they are available on request for the parts we quote you. Assemblies with threaded or bolted interfaces are additionally checked on a torque test rig.
Send a drawing as PDF, STEP, DWG or DXF, together with your annual volume and your SOP date. Our overseas business desk replies within 3 working days — either with a quotation, or with the specific list of questions we need answered before we can make one. You can upload the drawing directly through the RFQ form on this page.
No — not the frame itself. A front-seat structure is predominantly stamped sheet-metal panels, and large sheet-metal stamping is not a process we run. What we supply for a front seat are the wire and tube parts that mount on that structure: cushion support tubes, suspension wires, adjuster links, wire sub-assemblies and brackets. The complete frames we build are rear-seat cushion and back frames, which are wire and tube welded structures. If you are not sure which side of that line your part falls on, send the drawing and we will tell you before either of us spends time on a quotation.
Three separate lines, never one lump sum. (1) Part processing cost — material, bending, laser cutting and welding labour. (2) Tooling amortisation — fixture and gauge cost divided by the volume you commit to, quoted as its own line with the divisor stated, so you can recalculate it at a different volume. (3) Outsourced surface treatment — e-coat or zinc plating at the processor's rate. Any of the three can be challenged on its own.
A quotation from us is three separate lines, not one lump sum, so you can see exactly what you are paying for and challenge any of it:
Send a drawing (PDF, STEP, DWG or DXF) with your annual volume and SOP date. Our overseas business desk replies within 3 working days — either with a quotation or with the specific questions we need answered to make one.