Wuhan Yaxin Auto Parts Wuhan Yaxin Auto PartsSeat frame welded assemblies Send a drawing

HomeProducts

What we make

Three product families, all built around the same core: bend the wire or tube, cut and stamp the sheet-metal brackets, then weld it into one assembly the seat maker can bolt straight in.

Seat cushion wire frame assemblies

Our core product — the bent-wire and sheet-metal frame that carries the cushion foam and the occupant. A typical assembly starts as coiled wire, bent to profile on a CNC wire bender, combined with laser-cut and stamped sheet-metal brackets, and then welded by robot into a single rigid structure.

We supply these to Tier-1 seat makers as a finished, inspected assembly ready for foam-over on the seat-maker's line. The finished part sits between the foam cushion and the seat pan and must meet the seat maker's dimensional, weld, and fatigue specifications.

Example part: Y0494632B rear cushion wire frame assembly.

  • CNC wire bending to drawing Multi-axis benders, repeatable to drawing tolerance
  • Laser-cut and stamped brackets Sheet-metal inserts and gussets cut to net shape
  • Robotic MIG and spot welding 7 welding robots on arc and spot welding lines
  • Weld penetration reports on request Sectioned and etched samples per part number
  • IATF 16949:2016 certified scope Manufacture of seat frame assemblies

EPP frame assemblies

Wire frames designed around EPP foam — expanded polypropylene, the light, impact-absorbing material used in seat backs and headrests that must meet energy-management targets.

The wire frame inside an EPP part performs two jobs: it carries the foam mechanically during assembly, and it provides the fixing points to the seat structure. We form the wire profile to the mould geometry, weld in any required inserts or clips, and deliver the bare frame to the foam moulder.

Example part: Y0767438 LH EPP frame assembly.

  • Wire profile to mould geometry Formed to the EPP mould cavities of the seat maker's tooling
  • Insert welding Clips, nuts, and inserts welded in before foam-over
  • Matched to EPP moulder's schedule We co-ordinate lead times with the foam-over step

Tube & wire sub-assemblies, brackets

Not every programme needs a complete cushion assembly. We also supply the individual sub-components that go into a seat structure — either on their own or welded into the cushion assembly above.

  • Rear tubes and upright tubes Tube-bent to profile, ends upset or formed as required
  • Cushion support tubes Span the seat width and carry the cushion load
  • Necked-down tube assemblies Reduced-section ends for press-fit and swaged joints
  • Adjuster links Kinematic links for height and angle adjustment
  • Stamped brackets Laser-cut and press-formed mounting and connection brackets

These parts are quoted on the same three-line basis as a full assembly: part processing cost, tooling amortisation, and outsourced surface treatment each as a separate line.


The process chain behind every part

Everything from raw wire and tube to a welded, inspected assembly happens on our floor. Surface treatment (e-coat, zinc plating) is the one step we place with qualified outside processors — and we say so up front rather than implying we plate in-house.
  1. Wire & tube bending — Wire benders, 6+ tube benders, upsetting machines
  2. Laser cutting — Sheet-metal brackets and plates cut to net shape
  3. Piercing & flattening — Presses and hydraulic machines for end-forming
  4. Robotic welding — 7 welding robots, arc and spot welding lines
  5. Surface treatment — E-coat / zinc plating, placed with qualified outside processors
  6. Inspection — Torque test rig, weld penetration reports per part number
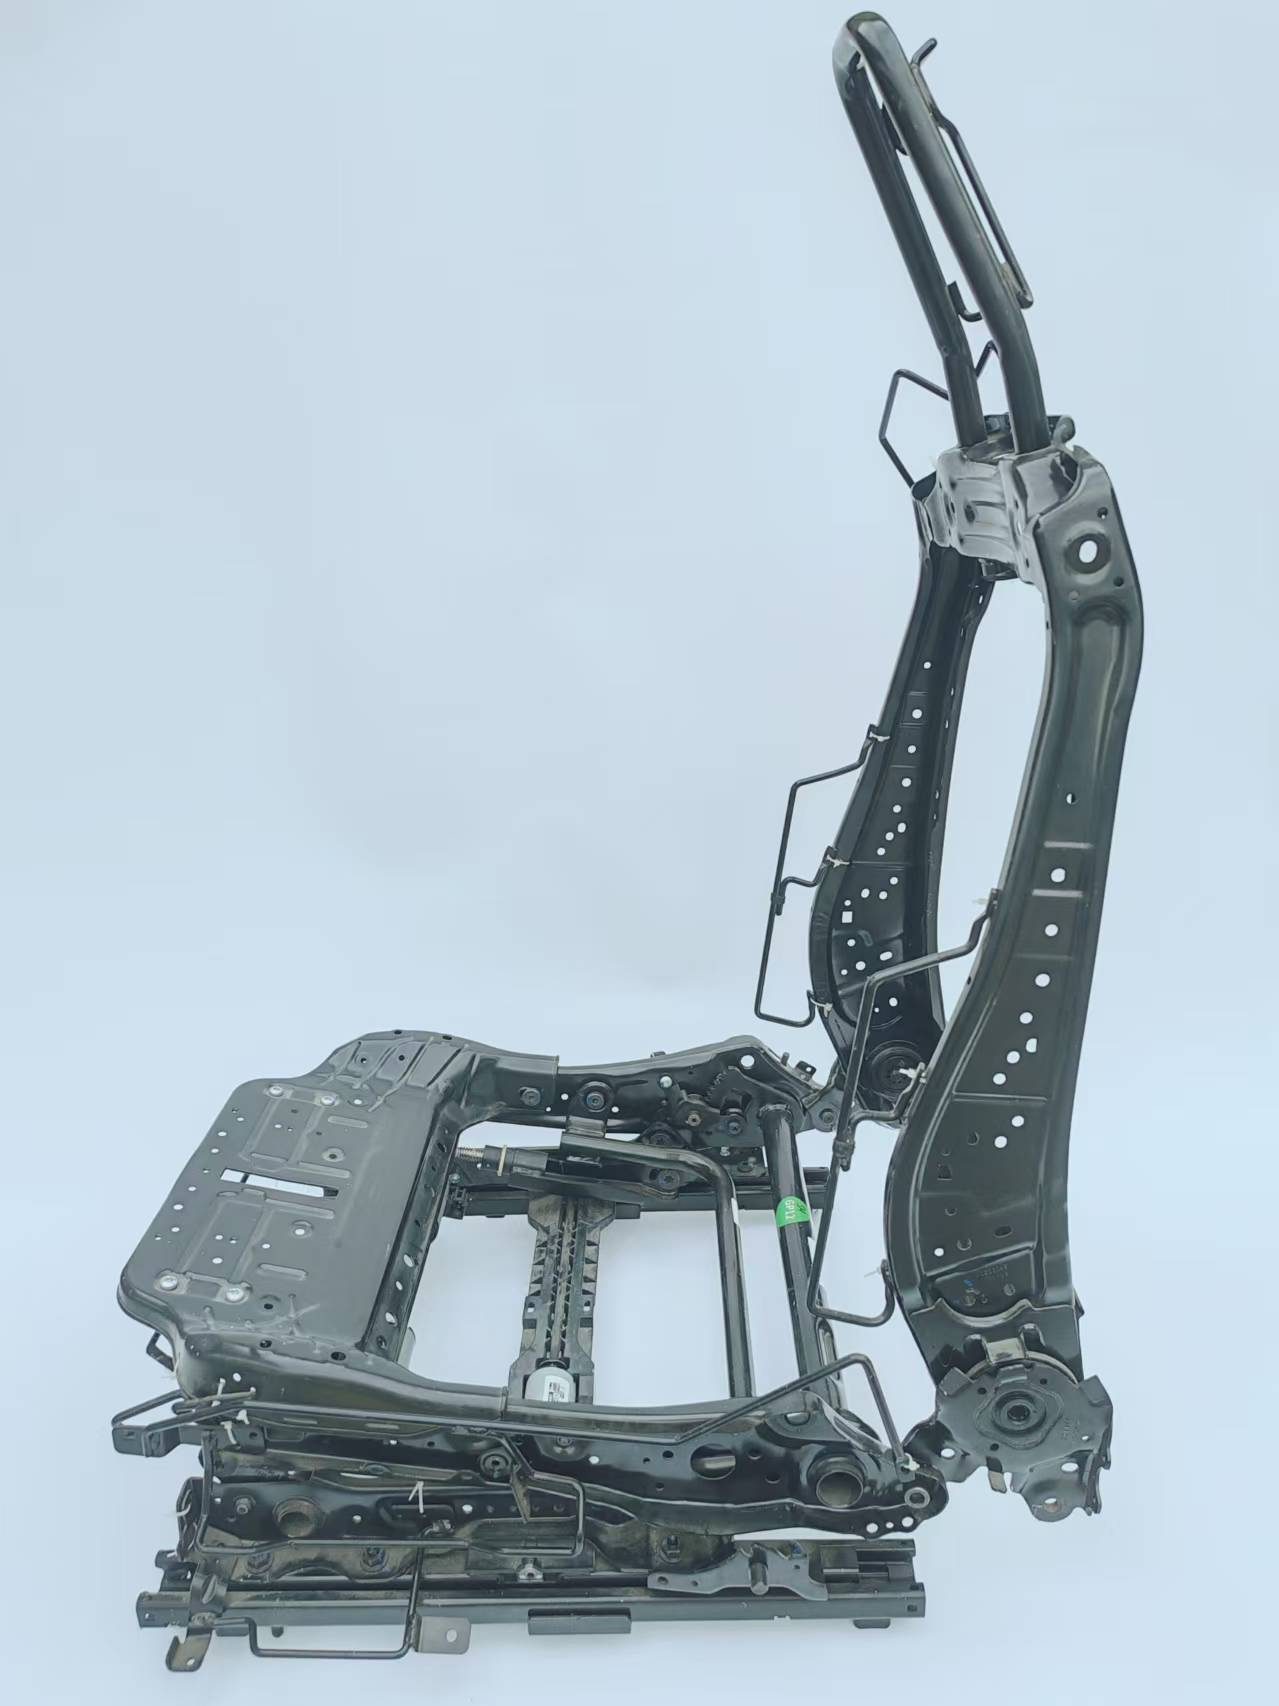
Welded seat frame assembly — actual production part
Welded seat frame assembly — actual production part. Every photo on this site is a real part we have made; we do not use stock factory imagery.

← Back to Wuhan Yaxin Auto Parts home