Rear-seat wire frame assemblies made to buyer drawing
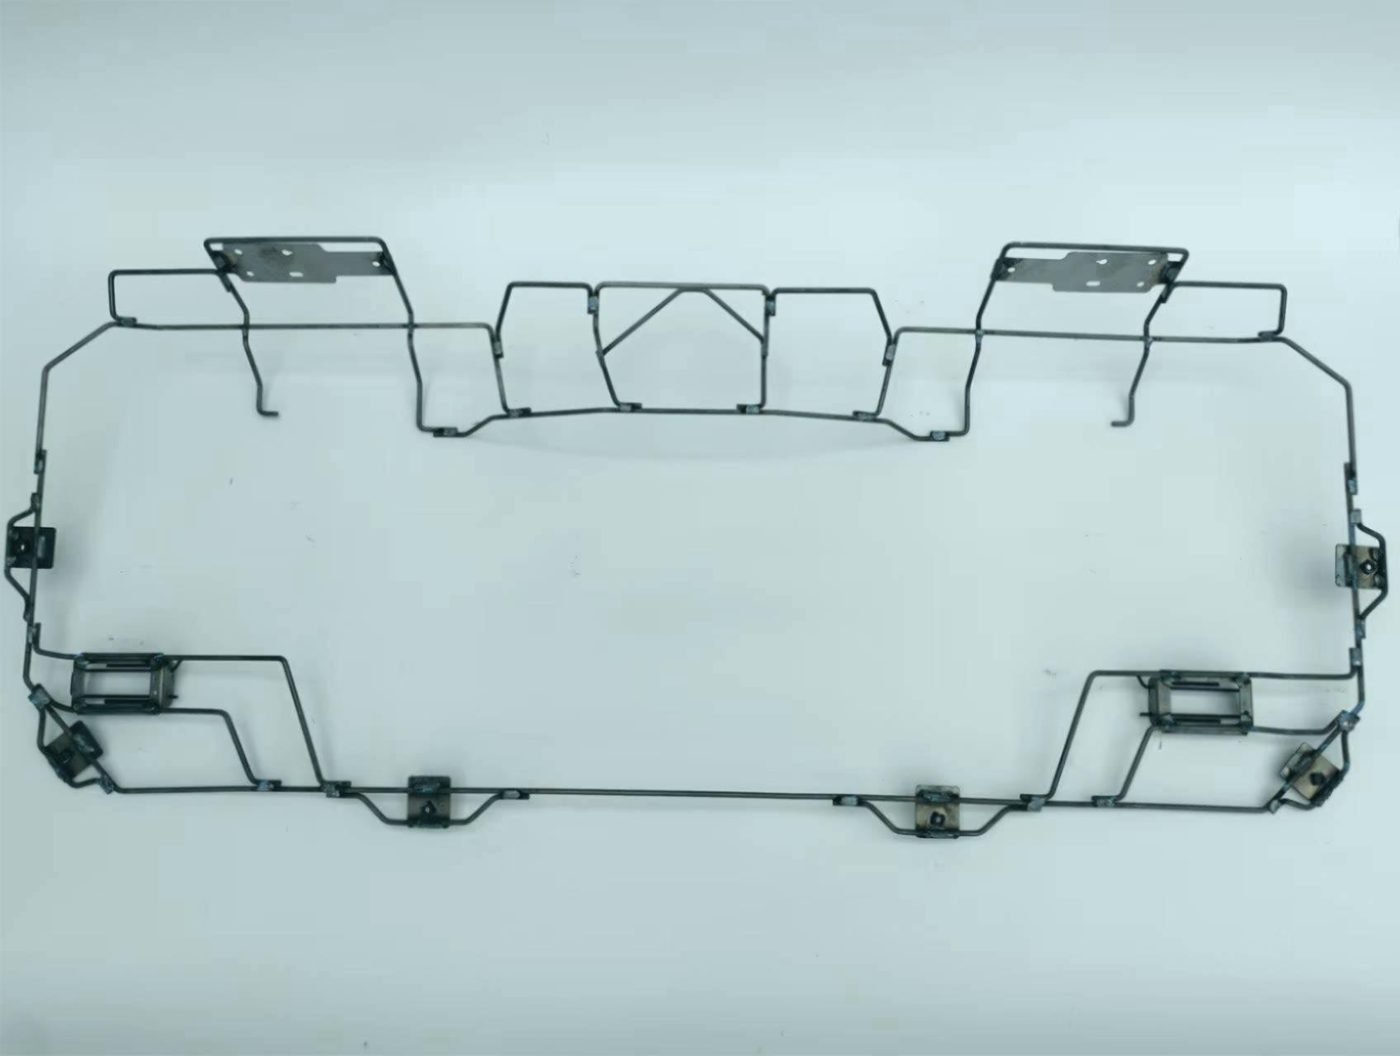
Wuhan Yaxin Auto Parts Co., Ltd. manufactures rear-seat wire and tube frame assemblies in Wuhan, China, to the buyer's drawing. Our scope is the metal structure: formed wire, bent tube, brackets, clips, welded nuts, checking gauges and welded assemblies under an IATF 16949:2016 quality system. We do not supply the foam pad, and we do not take ownership of the seat design.
What this page is about
A "rear-seat wire frame assembly" is easy to describe too broadly. On one RFQ it means a formed wire carrier under a cushion. On another it means a welded wire and tube structure with brackets, clips, welded nuts and gauge requirements. For sourcing, that difference matters, because the process set, the inspection method and the sample timing change with it.
So we describe the family by process and boundary, not by a vague seat-system label. We make the metal wire and tube structure to your drawing. We do not supply the polyurethane foam pad. We do not design the seat system. We do not present ourselves as the maker of the complete front-seat stamped structure. If the part is mainly formed wire, bent tube and welded attachments for a rear-seat cushion or back frame, it is in the right lane for us.
Manufacturing scope, and where it stops
Our forming window covers steel wire from φ2 to φ14 mm, and tube processing from φ8 to φ52 mm. The process set available to a rear-seat wire frame assembly can include wire forming, laser tube cutting, multi-station CNC tube bending, necking, hydraulic pressing, bracket preparation, welding, welded nuts and checking gauges.
The useful sourcing question is not only "can you make a wire frame?" It is: which parts of this assembly are inside your process window, which parts need a fixture, and which outside process must be quoted separately? Surface treatment is the most common example. If a drawing calls for e-coat, zinc plating or another finish, we say it plainly: surface treatment is outsourced and passed through as a separate process input. That honesty is better for both sides than hiding the gap until price freeze.
Welding and inspection evidence
Rear-seat wire frame assemblies often fail in the details: a weld nut pulls out, a bracket shifts in the fixture, a datum is not held, or the buyer asks for destructive weld evidence after the first price has already been discussed.
We have in-house weld penetration analysis (destructive testing) capability. For the parts we quote, weld penetration reports can be issued part number by part number on request. The acceptance figure belongs to your drawing, your referenced standard or your customer-specific requirement — we do not publish a house penetration number, because that would imply we weld to our own acceptance limit instead of yours. If you want to check whether a report you have been handed is usable, we wrote up what a weld penetration report has to say to be measurable, from the side that issues them.
A normal RFQ should therefore ask for weld callouts, datum points, restraint points, inspection frequency if known, and whether any destructive weld reporting is required before price is frozen.
Sample timing, and the shape of the quotation
For public statements we keep the timing facts conservative: wire formed samples can be as fast as 3 working days, while welded assemblies, seat frames and tube parts can be as fast as 10 working days. That is not a blanket promise. The useful answer depends on released drawing, material, fixture need, gauge need and inspection requirement.
Our quotation principle stays the same on every page of this site: the part processing cost, tooling or gauge amortisation, and outsourced surface treatment where applicable, each as its own line — see how we quote for why we refuse to send one lump-sum number. You can compare that structure. A lump sum hides the reason a price changes when volume, fixture or finish changes.
What to send first
For a rear-seat wire frame assembly RFQ, send:
- a PDF drawing for human review;
- STEP, DWG or DXF if the geometry is three-dimensional;
- wire diameter, tube diameter, material grade and finish requirement;
- annual volume and SOP timing;
- LH/RH information and whether the parts are mirrored;
- weld callouts, datum scheme and inspection requirement;
- sample timing and whether a checking gauge is expected;
- PPAP submission expectation, if any.
If PPAP is required, our current honest position: we prepare and submit PPAP to buyer requirement, and we have not yet made a PPAP submission directly to an overseas buyer. That line may feel uncomfortable. It is more credible than pretending a history we cannot document.
Why the narrow scope helps you
A narrow page should not feel small. It filters the right inquiry.
If you need a foam cushion pad, this is not the page. If the drawing is a complete front-seat stamped frame, this is not the page. If the drawing is a rear-seat metal wire or tube frame assembly to be made under a quality system, with welding and inspection evidence, then the next action is simple: send the drawing and the annual volume through the RFQ form.
The boundary also protects quotation speed. A supplier who tries to look like every seat-related factory attracts drawings we cannot price, and every wrong drawing steals time from a real fit. Saying "rear-seat wire and tube frame assemblies" lets you self-select before the first email. The result we want is not more unqualified traffic — it is fewer, sharper RFQs from buyers who already understand the process window, the outsourced finish boundary and the evidence we can provide.
Questions from buyers sourcing this assembly
Do you make the complete seat?
No. We manufacture the metal wire and tube structure to the buyer's drawing. The foam pad, trim, mechanism design and the complete seat system are outside this page's scope.
Can you make both wire and tube features in one rear-seat assembly?
Yes, if the geometry is within our published process window: wire from φ2 to φ14 mm and tube from φ8 to φ52 mm. The drawing decides whether the part needs wire forming, tube cutting, tube bending, brackets, welding, gauges or outsourced surface treatment.
Can you issue weld penetration reports?
Yes, for the parts we quote. We have in-house weld penetration analysis (destructive testing) capability and can issue reports part number by part number on request.
How fast can you make samples?
Wire formed samples can be as fast as 3 working days. Welded assemblies, seat frames and tube parts can be as fast as 10 working days, depending on released drawing, material, fixture, gauge and inspection needs.
Do you handle surface treatment?
Surface treatment is outsourced when required. It is quoted as a separate process input instead of being hidden inside a lump-sum part price.
Are you an IATF 16949 supplier?
We operate under an IATF 16949:2016 quality system. Certificate numbers, registration numbers and USI are not published on this website.
Send us the frame drawing.
Geometry, annual volume, SOP timing and inspection requirement through the RFQ form. We reply within 3 working days with either a quotation path or the specific missing information needed before a quotation can be made.