Bent tube seat frame sub-assemblies made to buyer drawing
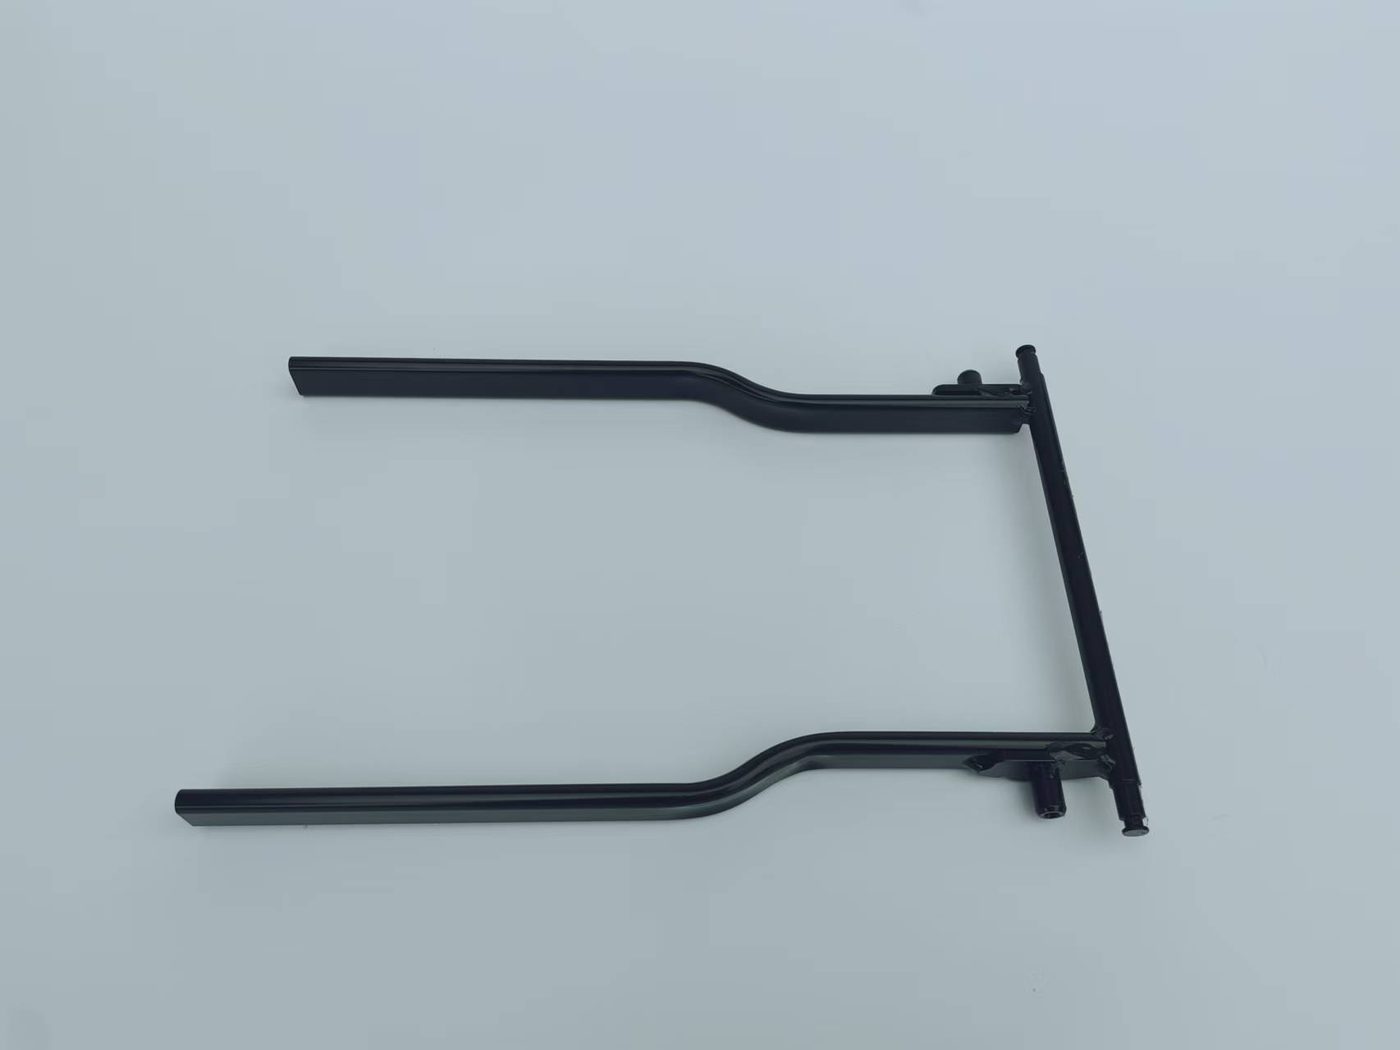
Wuhan Yaxin Auto Parts Co., Ltd. manufactures bent tube sub-assemblies for automotive seat structures in Wuhan, China, to the buyer's drawing. Our public tube processing window is φ8 to φ52 mm and can include laser tube cutting, CNC tube bending, necking, hydraulic pressing, welding, brackets, welded nuts, gauges and inspection under an IATF 16949 quality system.
What counts as a bent tube seat frame sub-assembly
A bent tube seat frame sub-assembly is usually not a complete seat frame. It is one metal structure inside your seat project: a bent tube support, a welded tube rail, a bracketed tube part, a cross member or a tube-and-wire assembly that later mounts into a larger seat system.
That boundary matters. We do not present this page as a complete seat-system offer. The correct scope is narrower and more useful: we manufacture metal tube and wire structures to your drawing. You own the seat design, the package space, the load case and the final seat validation. Our job is to make the specified metal part repeatably and to show the process evidence clearly.
Process window
Our public tube processing range is φ8 to φ52 mm. The process route can include automatic laser tube cutting, multi-station CNC tube bending, necking, hydraulic pressing, welding, brackets, clips, welded nuts, gauges and fixtures. If the part also contains formed wire, our public wire forming range is φ2 to φ14 mm.
For a buyer, the key question is not only whether the tube can be bent. It is whether the whole sub-assembly can be made without hiding a process gap. Your drawing may need a cut feature before bending, a formed tube end, a bracket weld, a nut, a gauge, and surface treatment after welding. Some of those steps are in-house. Surface treatment, where required, is stated plainly as outsourced and quoted as a separate process input.
What the drawing must make clear
For a tube sub-assembly RFQ, a simple picture is not enough. The supplier needs the tube diameter, wall thickness, material grade, bend radii, end-forming details, hole positions, bracket locations, weld callouts, datum scheme and surface treatment requirement. If a 3D model exists, send it with the PDF drawing, because bend sequence and handedness are easy to misunderstand from a flat image.
The RFQ should also say whether the part is left-hand, right-hand or mirrored. That one line can change the fixture discussion. If a checking gauge is expected, say so at the first RFQ stage instead of after the unit price is discussed.
Welding and inspection
Bent tube sub-assemblies often fail at the interfaces: a bracket angle, a welded nut, a hole location after springback, or a tube end that no longer matches the gauge after welding heat. For automotive seat projects, inspection cannot be reduced to "looks acceptable."
We have in-house tensile testing, torque fatigue testing and weld penetration analysis (destructive testing) capability. For the parts we quote, weld penetration reports can be issued part number by part number on request. The acceptance criteria still belong to your drawing, referenced standard or customer-specific requirement — we do not publish a universal weld penetration number. If you want to check whether a report you have been handed is usable, we wrote up what a weld penetration report has to say to be measurable, from the side that issues them.
Sample timing and quotation structure
The approved public timing is that welded assemblies, seat frames and tube parts can be as fast as 10 working days. That is a sample possibility, not a blanket launch promise. Drawing release, material, fixture need, gauge need and inspection requirement can all change the answer.
The quotation should remain understandable. Our public quotation story separates part processing cost, tooling or gauge amortisation, and outsourced surface treatment where applicable — see how we quote. That structure helps you see why the price changes when annual volume, finish or fixture requirement changes.
What to send before asking for price
For a bent tube seat frame sub-assembly, send:
- a PDF drawing for notes, tolerances and weld callouts;
- STEP, DWG or DXF when the geometry is three-dimensional;
- tube diameter, wall thickness and material grade;
- bend radii, end-forming and hole requirements;
- bracket, clip and welded-nut details;
- annual volume, SOP timing and sample deadline;
- LH/RH or mirrored-part information;
- surface treatment requirement;
- weld inspection and gauge requirement;
- PPAP expectation, if any.
If PPAP is required, we keep the honest public line: we prepare and submit PPAP to buyer requirement, and we have not yet made a PPAP submission directly to an overseas buyer. That sentence prevents a later trust problem. It also tells you to raise PPAP expectations early, before the quotation becomes a fixed promise.
Why the narrow lane helps you
Generic tube bending pages usually talk about equipment. Generic seat frame pages often talk about the complete seat. This page sits between those two lanes: automotive seat tube sub-assemblies, made to drawing, with welding, gauges, inspection and a clear process boundary.
That is the right shape for a new B2B site. We are not trying to rank for every tube bending search. We are trying to be a credible answer when you search for a China supplier who understands the metal tube part inside an automotive seat project and can quote from a real drawing without pretending to own the whole seat system.
Questions from buyers sourcing tube sub-assemblies
What tube sizes can you process?
Our public tube processing window is φ8 to φ52 mm. The exact answer depends on material, wall thickness, bend radius, cut features, fixture need and inspection requirement.
Do you make complete seat systems?
No. We manufacture metal wire and tube structures to the buyer's drawing. Foam pads, trim, complete seat systems and buyer-owned seat design are outside this page's scope.
Can a tube sub-assembly include brackets or welded nuts?
Yes, where the drawing is in scope. The process route can include laser tube cutting, CNC tube bending, welding, brackets, clips, welded nuts, gauges and fixtures.
Can you issue weld penetration reports?
Yes, for the parts we quote. We have in-house weld penetration analysis (destructive testing) capability and can issue reports part number by part number on request.
How fast can tube samples be made?
Welded assemblies, seat frames and tube parts can be as fast as 10 working days, depending on drawing release, material, fixture, gauge and inspection needs.
Is surface treatment in-house?
Surface treatment is outsourced when required and should be quoted as a separate process input instead of being hidden inside a lump-sum price.
Send us the tube drawing.
Geometry, annual volume, SOP timing, sample deadline and inspection requirement through the RFQ form. We reply within 3 working days with either a quotation path or the specific missing information needed before a quotation can be made.